





160 Parallel Twin Screw Change SOP
Professional Screw Replacement Procedure for Stable SPC Flooring Production
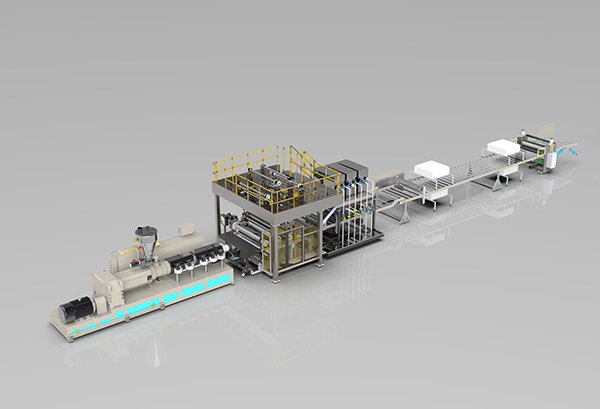
Reliable extrusion performance begins with proper maintenance. As one of the most critical components in an SPC flooring production line, the parallel twin-screw extruder directly influences plasticizing efficiency, product quality, production stability, and equipment lifespan. To perform every maintenance operation with maximum precision, our engineering team follows a standardized 160 parallel twin-screw change SOP.
This document provides an overview of the professional workflow followed during the replacement of screws and barrels on a 160 parallel twin screw extruder. Our experienced service engineers perform every operation using precision measuring instruments and standardized installation methods, ensuring optimal alignment, reliable operation, and long-term production stability.

Note: Start installing from the discharge port. Position 1 is the discharge port, and the two heaters should not be installed.
Tools for Screw Change
The following professional tools are prepared before maintenance begins:
- Crowbar
- Vernier caliper
- Dial indicator
- Allen wrench
- Pipe wrench
- Feeler gauge
- Blade ruler
- Other professional maintenance tools
A complete set of precision tools ensures accurate measurement, proper alignment, and safe installation throughout the maintenance process.
Prepare Work Before Change
Before replacing the screw and barrel assembly, a complete inspection is performed to ensure the machine is ready for maintenance.
The preparation procedure includes:
- Record barrel and screw S/N
All barrel and screw serial numbers are recorded for future maintenance history and spare parts traceability.
- Check twin screw relative position
The relative position of the twin screws is carefully inspected to confirm proper synchronization before disassembly.


- Check no foreign material inside barrel
Inspect the barrel interior to clear any foreign material that could interfere with removal or damage new components.
- Check no damage on copper cooling water pipe
The cooling system is inspected to verify that all copper cooling water pipes remain intact before maintenance begins.
Part 1 – Change Screw and Barrel
Step 1
Close vacuum pump and cooling water of vacuum pump.
The vacuum system is shut down before any mechanical work begins to ensure safe maintenance conditions.

Step 2
Move the calender to the shearing machine for about 1 meter as the operating space for screw & barrel replacement.
Adequate working space is created to allow safe removal and installation of the screw and barrel assembly.

Step 3
Separate from the connecting barrel of the combiner core and check whether the top of the screw is in the same plane. If not, it means that the screw is broken.
The combiner connection is separated and the screw position is inspected to determine its operating condition before removal.

Step 4
Keep the barrel temperature, try to turn on the main engine at a lower speed, and remove the residual materials in the screw.
Residual material inside the screw is discharged as much as possible to simplify the replacement process.
Step 5
If it is unable to discharge, prepare special tools and push the screw out of the barrel.
Special maintenance tools are used whenever normal discharge cannot remove the remaining material.
Step 6
If the special tools cannot be ejected, prepare a new set of barrel and screw and replace them as a whole.
If necessary, the entire screw and barrel assembly is replaced to restore production performance.
Step 7
Cool down the barrel, remove the cooling water pipe, heating line, force feeding, and separate the flange between the screw and the distribution box.
All auxiliary systems are disconnected before mechanical removal begins.

Step 8
use the top handle of the barrel to separate the barrel from the distribution box (clean the lubricating screw rod and rail before use), and be careful whether the barrel moves synchronously with the support. If the bracket moves but the barrel does not move, use a crowbar to separate the barrel flange from the distribution box flange
Proper movement of the barrel support is confirmed to prevent equipment damage during removal.


Step 9
When the barrel position meets the lateral displacement, use the bottom rocker to move the barrel out laterally so as to prepare operation space for screw & barrel change.
The barrel is shifted sideways to provide sufficient maintenance access.

Step 10
Lift and place the screw barrel on the machine platform as a whole.
The complete assembly is safely removed using suitable lifting equipment.

Step 11
Use the bottom rocker to move the barrel to the center line of the distribution box, and then use the top handle to move the barrel to close to the joint surface of the distribution box, and preliminarily adjust the barrel level. Measure the gap from the highest point and the lowest point inside the distribution box with a feeler gauge.
If not, pad up (use gasket or cushion block) or reduce (need to machine the upper plane of the support) the barrel height Degree. Use the bottom rocker to adjust the barrel level so that the barrel can enter the joint surface of the distribution box.
The barrel is carefully positioned to achieve accurate alignment before installation.


Step 12
Push the barrel into the joint surface of the distribution box with the front-end crank until one side of the barrel flange is just in contact with the flange of the distribution box (ensure that the barrel support is vertical to the barrel in the whole process).
Use a feeler gauge to measure the gap between the upper, lower, left and right planes of the barrel flange and the plane of the distribution box. By adjusting the height of the screw tip bracket (add gasket or copper sheet, the ratio of the clearance between the feeler gauge and the thickness of the gasket is about 1:10; that is, the clearance measured by the feeler gauge is 0.1 mm, and the gasket needs to be increased by 1 mm). The clearance between the left and right sides is adjusted by the side crank.
Finally, the flange plane of the barrel is parallel to the plane of the distribution box, and the barrel is shaken in and out twice to ensure that the joint surface of the barrel and the distribution box fits normally, and the in and out is smooth. A flange screw is fixed at the top, bottom, left and right respectively.
Precision alignment is performed to ensure smooth engagement between the barrel and gearbox.

Step 13
Manually turn the motor (clockwise to make the upper plane of the output shaft of the distribution box vertical upward), and then install the spline sleeve after the marking position of the spline sleeve is also vertical upward. Use the pipe wrench to rotate the screw to the upper end face vertically.
Next, use a crowbar to push the screw into the spline sleeve until the end face of the screw shank sits flush against the distribution box’s output shaft.
The drive connection is installed and aligned before final positioning.

Step 14
Press the screw tip at the discharge end of the barrel with tools (lifting lug and crowbar), pry the other screw with a screwdriver or crowbar to make it move forward and backward in series. Measure at the outlet end with vernier caliper or dial indicator, and record the clearance between the two screws.
Turn the motor manually to make the screw rotate 120 degrees and 240 degrees in the positive direction, and record the corresponding clearance value (a1a2a3). In the same way, measure and record the clearance between the two screws (b1b2b3).
The formula for calculating the clearance adjustment value is (((a1 + A2 + a3) / 3) – ((B1 + B2 + B3) / 3)) / 2. Move out the barrel, remove the screw shank gasket cover, and adjust the thickness of the gasket at the top of the screw spline to make the error of the two screws in series less than 0.2mm
Take multiple measurements to ensure synchronized screw movement and reliable power transmission.

Step 15
Move the barrel into the distribution box again and measure the relative movement between the two screws again to confirm whether the difference is within 0.2 mm.
Verification measurements confirm that installation accuracy meets engineering standards.

Step 16
Press the screw tip at the discharge end of the barrel with tools (lifting lug and crowbar) to make the top plane of two screw spline close to the shaft plane of distribution box. Use tools (caliper or dial indicator) to measure the actual position of two screws on the barrel, and adjust the thickness of gasket to achieve the ideal position.
Fine adjustment is completed to achieve precise installation.

Step 17
Check whether the relevant fixing screws of the barrel screw are tightened.
All fasteners are inspected before restarting the machine.
Step 18
Installation of combiner core, mold, heating block, cooling water pipe, forced feeding, etc.
All auxiliary equipment is reinstalled after alignment is completed.
Step 19
Warm up and start up.
Once all inspections are complete, heat the extrusion system and resume production.
Part 2 – Replace Screw
When replacing only the screw while keeping the barrel, follow this standardized procedure.
Step 1
Close vacuum pump and cooling water of vacuum pump.
Step 2
Move the calender to the shearing machine for about 1 meter as the operation space for barrel replacement.
Step 3
Separated from the position of combiner core connecting barrel.
Step 4
Check whether the top of the screw is in the same plane. If not, it means that the screw is broken.
Step 5
Keep the barrel temperature, try to turn on the main engine at a lower speed, and remove the residual materials in the screw.
Step 6
If it is unable to discharge, prepare special tools and push the screw out of the barrel.
Step 7
Discharge all materials from the barrel, then cool the barrel down. Next, disconnect the cooling water pipes, heating lines, and force feeder, and separate the flange between the screw and the distribution box.
Step 8
Use the top handle of the barrel to separate the barrel from the distribution box (clean the lubricating screw rod and rail before use), and be careful whether the barrel moves synchronously with the support. If the bracket moves but the barrel does not move, use a crowbar to separate the barrel flange from the distribution box flange.
Step 9
When the barrel reaches the required lateral displacement position, use the bottom rocker to move the barrel outward laterally, creating sufficient space for barrel replacement.
Step 10
Use crowbar, crane and forklift to take out the screw from the barrel.

Step 11
Install the new screw into the barrel.
Step 12
Adjust the height of the bracket at the discharge port of the barrel to make the straight section of the barrel smooth in and out of the distribution box.
Step 13
Leave a gap of about 0.3mm between the barrel flange and the plane of the distribution box. Use a feeler gauge to measure the gap between the upper and lower plane of the barrel flange and the plane of the distribution box. First, adjust the height of the mold-side bracket until the face of the barrel flange sits completely parallel to the distribution box plane. Once aligned, securely tighten the flange screws.
Step 14
First, install the spline sleeve to connect the distribution box shaft to the screw shank. Next, stand at the discharge end of the barrel and push against the screw tip using a crowbar so that the face of the screw splines sits flush against the distribution box shaft.
Step 15
Fix one screw, pry another screw with a screwdriver or crowbar, and move it forward and backward in series. Use a vernier caliper to measure at the outlet end, and record the serial clearance. Next, measure and record the axial play (float) of the second screw using the exact same procedure. Then, adjust the shim thickness at the top of the screw splines so that the clearance difference between the two screws remains less than 0.2 mm.
Step 16
Press the screw tip at the discharge end of the barrel with a tool (lifting lug and crowbar) to make the top plane of the two screw splines close to the axis plane of the distribution box. Measure the actual position of the two screws on the barrel with a tool (caliper or dial indicator) to reach the ideal position by adjusting the thickness of the gasket.
Step 17
Check that all fasteners securing the barrel and screw are tight.
Step 18
Installation of combiner, mould, heating block, cooling water pipe, forced feeding, etc.
Step 19
Warm up and start up.
Professional After-sales Service
A qualified screw replacement goes far beyond simple component replacement. Accurate measurement, precise alignment, standardised workflows and professional engineering support are all critical to sustaining stable and long-term extrusion operation.
Our service engineers adhere to strict standard operating procedures for all maintenance projects. This ensures stable equipment performance, minimised downtime, prolonged component service life, and consistent SPC flooring production quality. We comply with professional engineering standards for all operations, including full screw and barrel assembly replacement and routine screw maintenance, delivering reliable production outcomes for global customers.


 Head Office
 Our Tel
 Our Email

